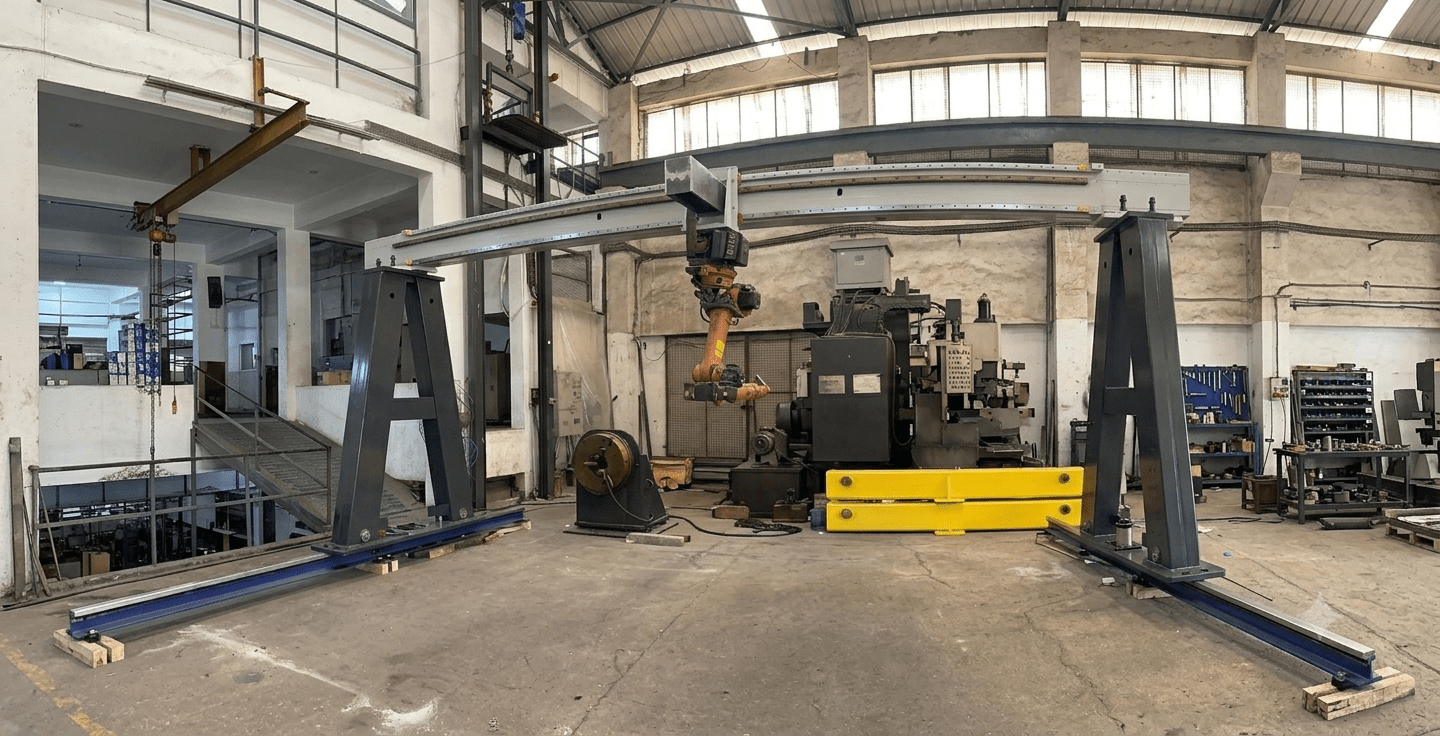
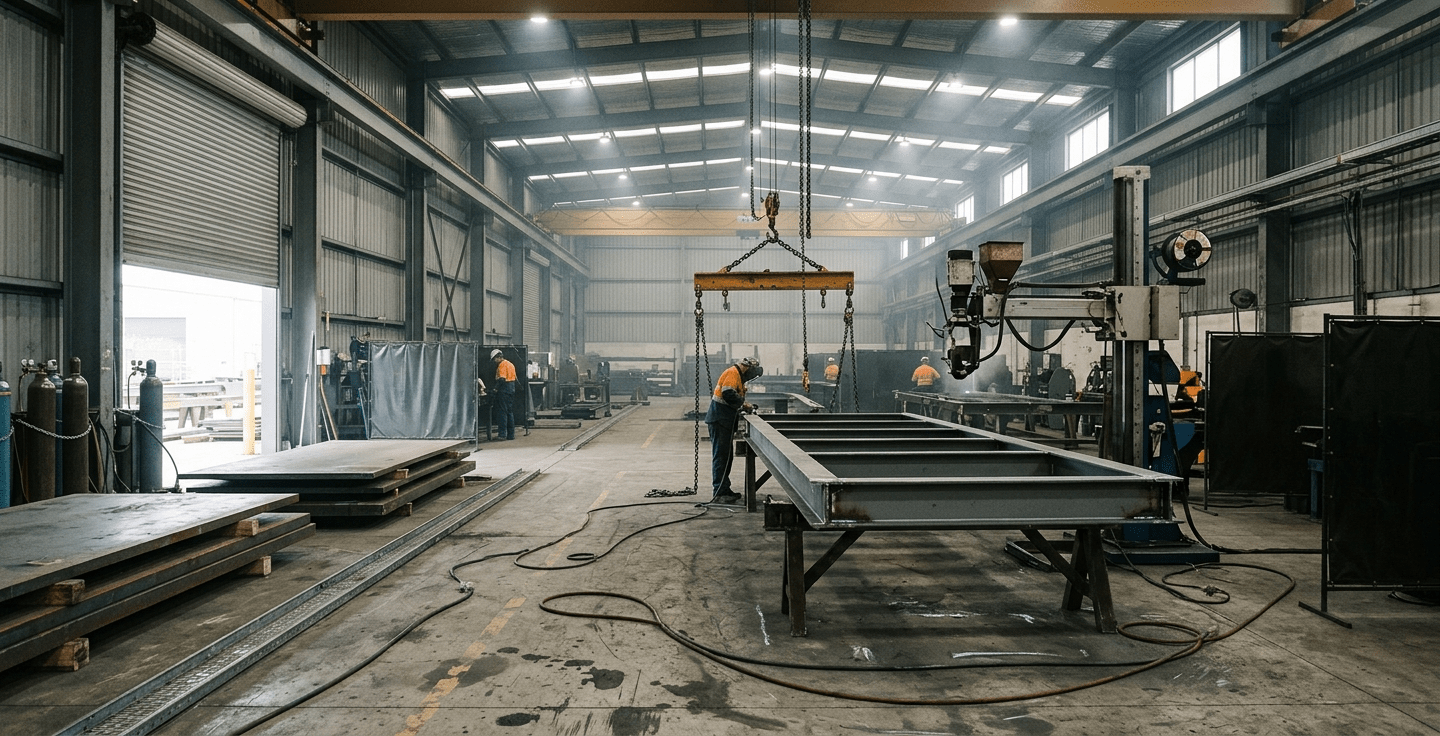
A hull block welding gantry holds position at ten-ton scale while the weld runs metres across curved plate in open yard conditions. That is why shipbuilding welding automation is built differently. Hull panels carry 12 to 16 metres of butt and fillet welds per block, stiffeners sit at tight pitch with one-sided access, and every seam is inspected to classification society rules. As a result, the system must deliver stable arc parameters across long travel with real-time seam tracking. That is the production environment Drupe builds for.
Approved supplier to L&T, Godrej and heavy structural fabricators across India. Every system is engineered and fabricated at our 300-ton MIDC Taloja floor, sized for the throughput shipyard production demands.
Key Capabilities
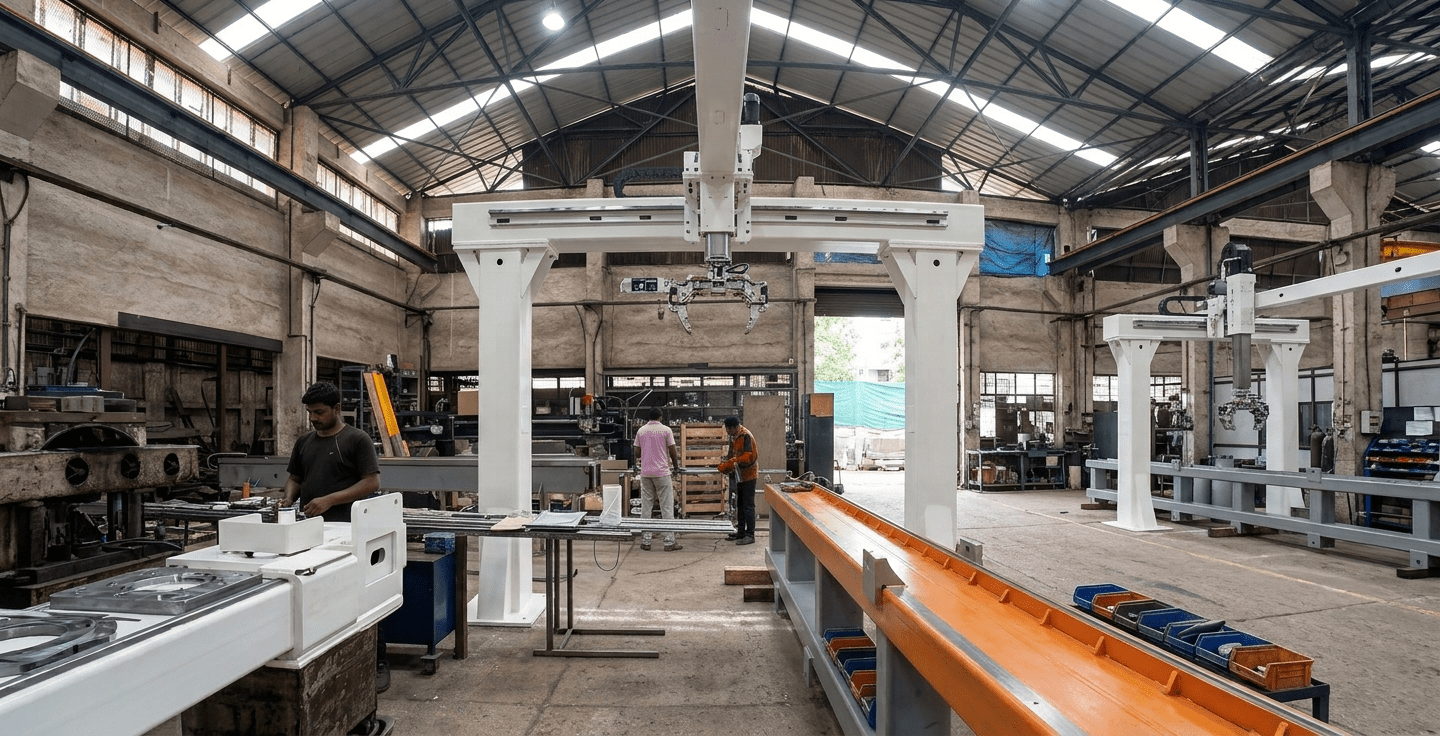
1. Robotic Hull Block Welding Gantries Overhead gantries carrying six-axis robots with envelopes up to 20,000 x 6,000 x 3,000 mm, built around your block size and bay layout. Camera-based seam tracking compensates for fit-up variation in real time.
2. Long Linear Tracks for Panel Lines 7th-axis robot tracks with strokes up to 20,000 mm and payloads up to 5,000 kg. Track, clamps and support units built in-house and matched to existing yard steelwork.
3. CNC Plate and Bevel Cutting Gantry and table-type CNC machines with Hypertherm plasma and oxy-fuel. Drupe’s Gen-3 bevel head delivers bevel prep in the same pass as the profile cut.
4. Flex Track for Curved Hull Seams Portable magnetic-mount rail for curved seams where a fixed gantry cannot reach. Holds consistent standoff on double-curved plate for MIG/MAG and submerged arc.
5. Rail Clamps and Support Units Precision-ground clamps, support units and pinion assemblies rated for yard-scale load. Same components inside every Drupe gantry, available separately.
Planning & Strategy
From your first drawing to lifetime service, every project runs the same disciplined path.
Application Study
In-house Manufacturing
Design & Approval
Factory Acceptance Testing
On-site Commissioning
AMC & Lifetime Support
Ideal For
Hull block panel butt and fillet welding
Stiffener and web frame attachment welding
Deck and bulkhead panel assembly
Double-bottom and double-hull block fabrication
Curved hull plate seam welding
Profile and bevel cutting for block parts
Heavy component transfer between cutting, welding and assembly bays
Sub-assembly welding for brackets, lugs and foundations
Why Drupe?
In shipbuilding, a hull block welding gantry has to work in yard conditions: open bays, dust, temperature swings and plate that is never perfectly flat. As a result, the automation has to be robust enough to hold weld parameters while the environment fights it. Drupe has already built for that environment: for example, our gantries carry robots across 20-metre spans at ten-ton scale with sub-millimetre repeatability, and our linear tracks run the full length of a panel line without losing position.
In addition, because the gantry structure, the track, the controls and the peripherals are all engineered and fabricated in-house at MIDC Taloja, any problem on site is handled end to end by one team. Our approved supplier standing with L&T and Godrej means our systems have already cleared the procurement audits heavy-industry buyers run. Engineered, commissioned and supported in India by a 150-person team, with proven hull block welding gantry systems already running on Indian production floors.
Frequently Asked Questions
How do you handle the distortion control that classification societies require on thin hull plate?
The system is engineered for low-distortion welding first: controlled travel speed, stable heat input and fixed torch positioning reduce the variables that cause distortion on thin stainless and mild steel plate. Because the gantry holds the robot at a consistent standoff across the full panel, heat input stays within the qualified range seam after seam. Weld data capture can be integrated where your QA process or the classification society standard requires it. We work to your WPS and inspection regime rather than asking you to change it.
Can you weld curved hull seams and contoured plate as well as flat panels?
Yes. For flat and lightly curved panels, the gantry system with seam tracking handles the work. For double-curved plate and areas the gantry cannot reach, our flex track system mounts magnetically to the hull surface and holds the torch at a consistent standoff and travel speed. As a result, the same yard can automate both flat block assembly and curved hull seams without bringing in a second supplier.
Can the system scale if our block sizes or throughput targets change later?
Yes. Because the gantry, the track and the controls are all built by Drupe, extending a track run, adding a second robot station or widening the gantry span is an engineering change on an existing platform, not a new procurement. We design the initial system with expansion in mind so that adding capacity later does not require rebuilding the structure.
We are always ready to help you and answer your questions.
Contains information related to marketing campaigns of the user. These are shared with Google AdWords / Google Ads when the Google Ads and Google Analytics accounts are linked together.
90 days
__utma
ID used to identify users and sessions
2 years after last activity
__utmt
Used to monitor number of Google Analytics server requests
10 minutes
__utmb
Used to distinguish new sessions and visits. This cookie is set when the GA.js javascript library is loaded and there is no existing __utmb cookie. The cookie is updated every time data is sent to the Google Analytics server.
30 minutes after last activity
__utmc
Used only with old Urchin versions of Google Analytics and not with GA.js. Was used to distinguish between new sessions and visits at the end of a session.
End of session (browser)
__utmz
Contains information about the traffic source or campaign that directed user to the website. The cookie is set when the GA.js javascript is loaded and updated when data is sent to the Google Anaytics server
6 months after last activity
__utmv
Contains custom information set by the web developer via the _setCustomVar method in Google Analytics. This cookie is updated every time new data is sent to the Google Analytics server.
2 years after last activity
__utmx
Used to determine whether a user is included in an A / B or Multivariate test.
18 months
_ga
ID used to identify users
2 years
_gali
Used by Google Analytics to determine which links on a page are being clicked
30 seconds
_ga_
ID used to identify users
2 years
_gid
ID used to identify users for 24 hours after last activity
24 hours
_gat
Used to monitor number of Google Analytics server requests when using Google Tag Manager